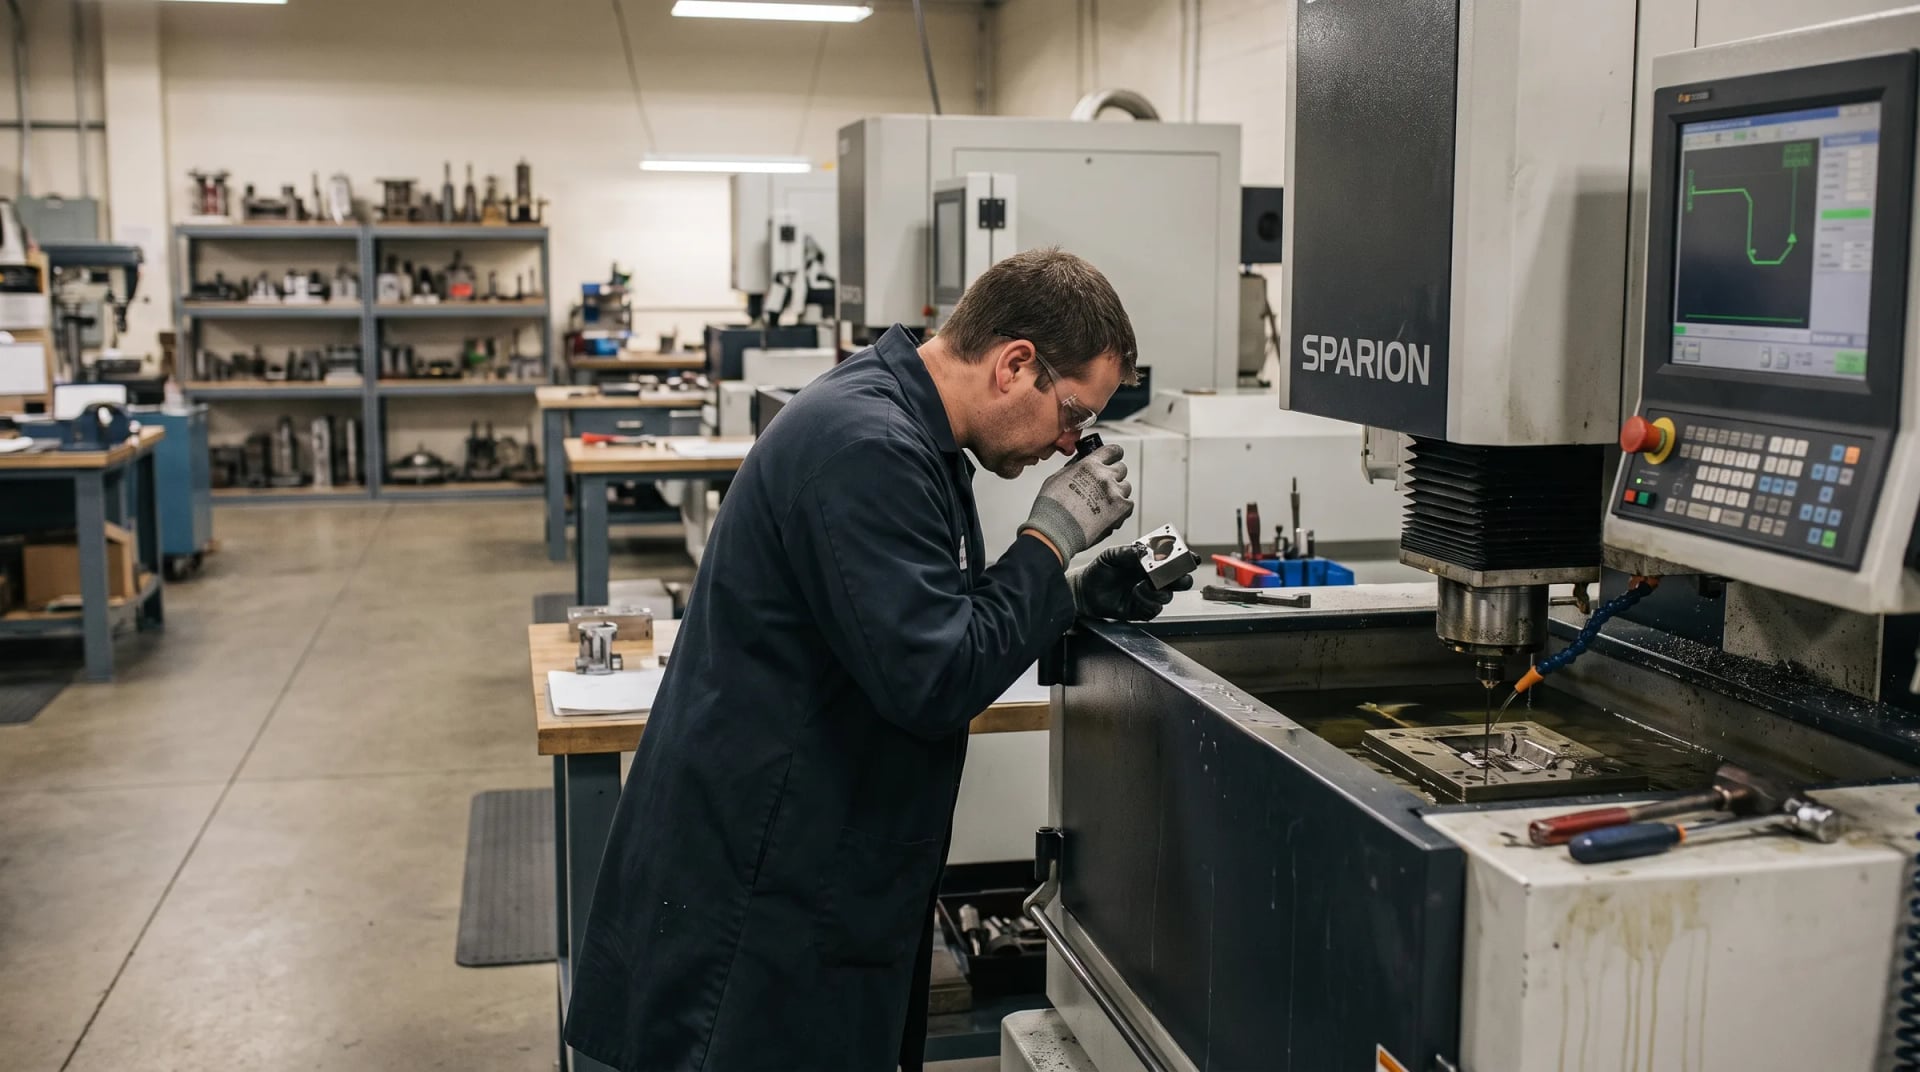
EDM (Wire & Sinker)
Cut what a tool can't touch — hardened steel, deep cavities, mirror finishes.
2 Processes
Wire & Sinker
Ra 0.05 μm
Best Surface Finish
±30°
Max Wire Taper Angle
Not sure which edm (wire & sinker) is right for you?
Our AI can help you compare machines, find parts, and explore your options.
Advantages
Why Choose EDM (Wire & Sinker)?
Cuts What Cutting Tools Can't
Hardened tool steel, carbide and exotic alloys erode the same regardless of hardness.
Mirror-Grade Finishes
Fine-finish passes reach Ra 0.05-0.1 μm, often eliminating a secondary polishing step.
Distortion-Free on Delicate Parts
No mechanical cutting force means thin or hardened sections stay true to print.
Full Dielectric System Support
Installation, training and ongoing service cover both water and oil dielectric systems.
Featured
SW-400
Precision wire EDM with automatic threading, cutting hardened tool steel to a mirror finish.
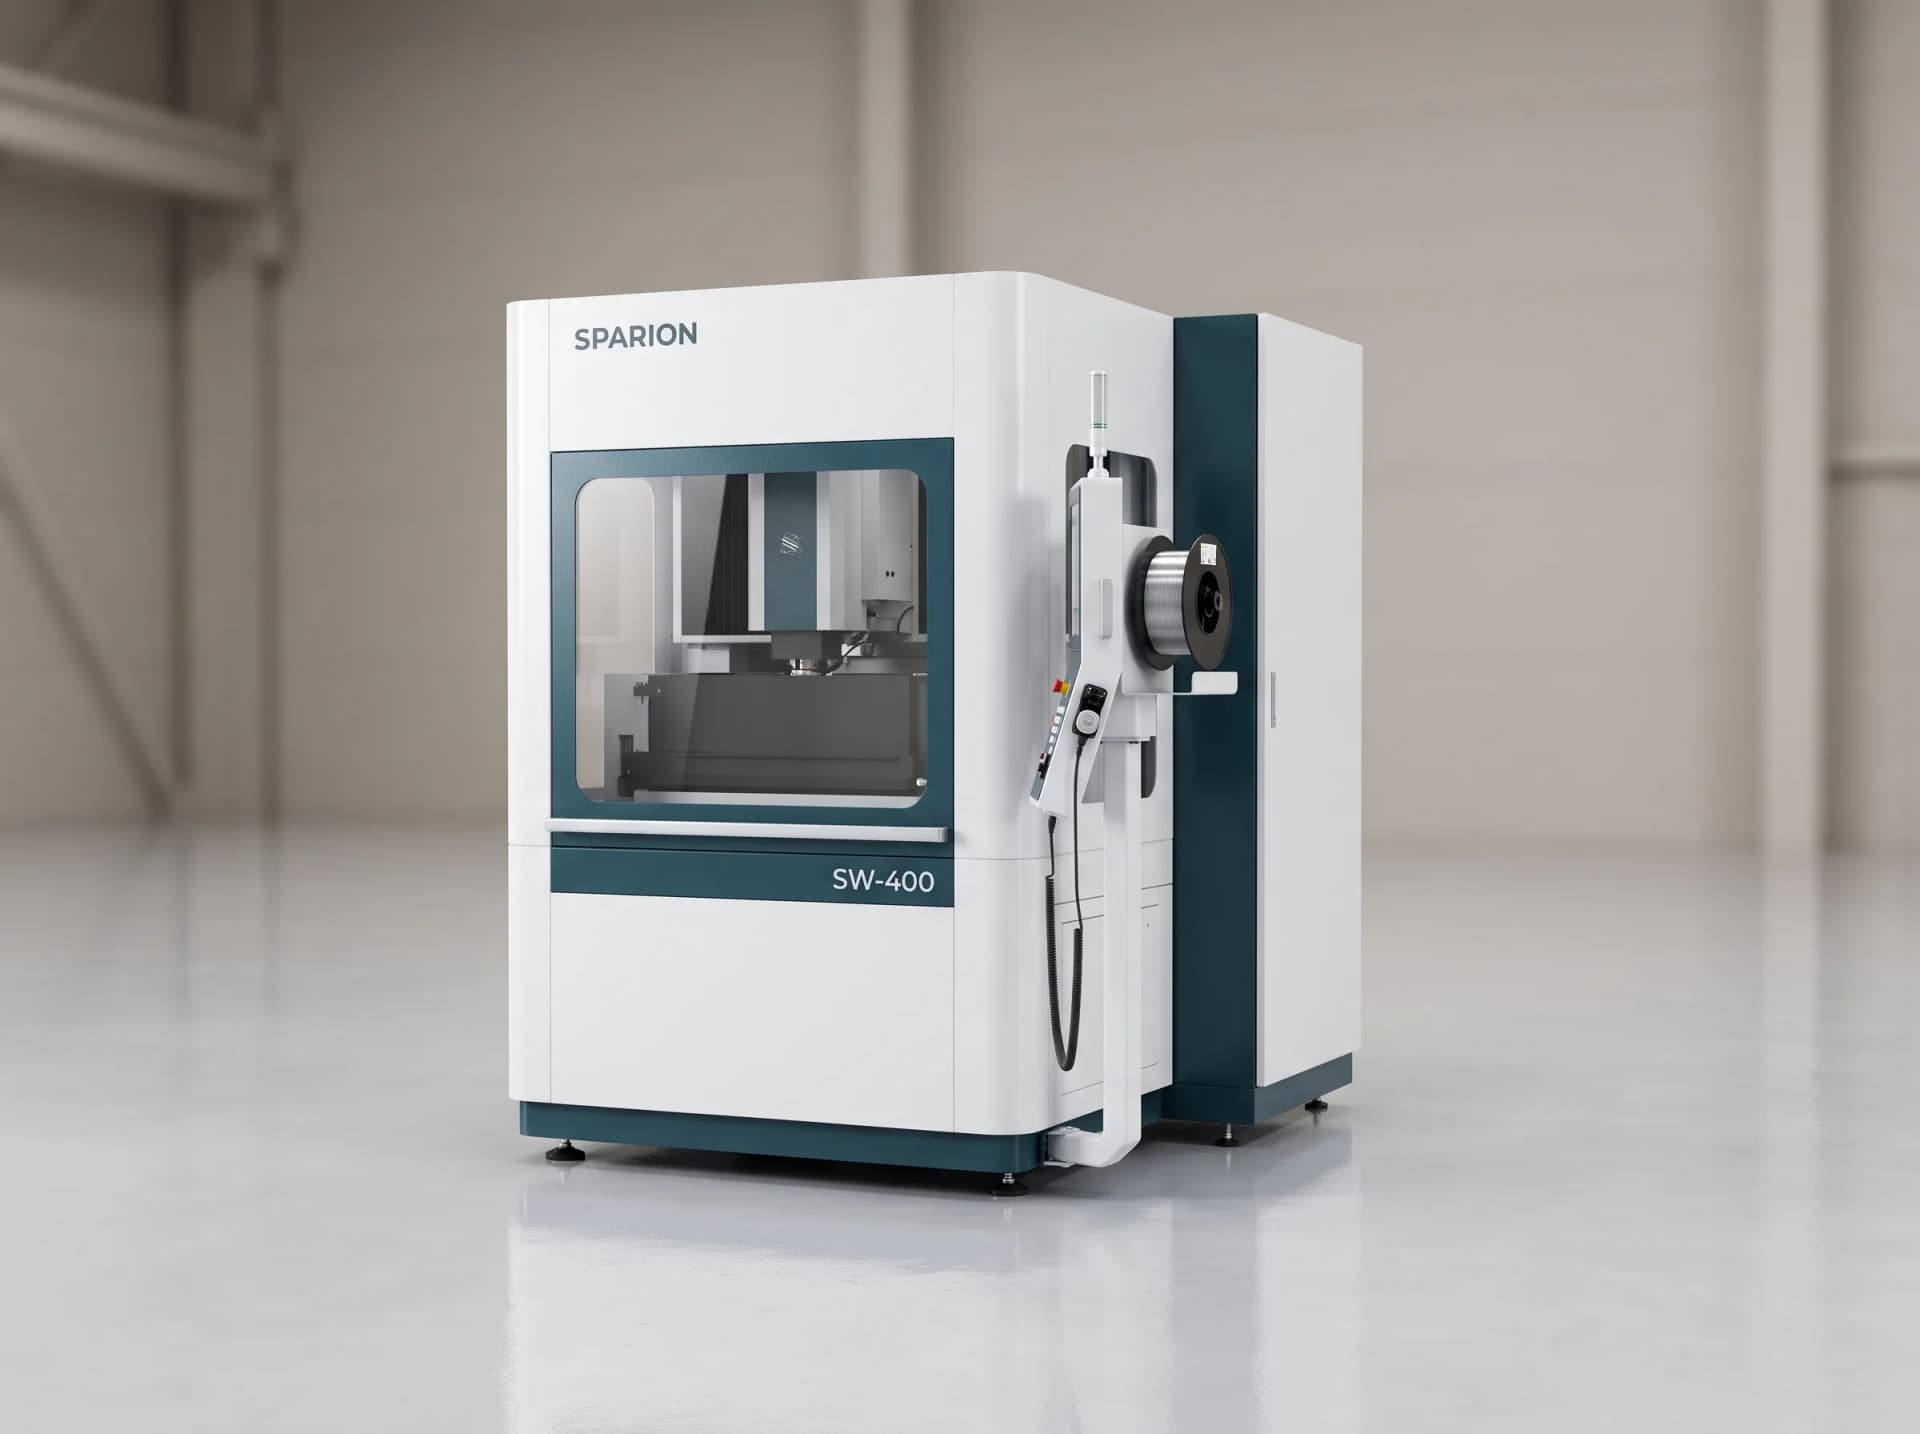
Sparion SW-400
Max workpiece size
650 x 450 x 250 mm (25.6 x 17.7 x 9.8 in)
Max workpiece weight
400 kg (882 lb)
X / Y / Z travel
400 x 300 x 250 mm (15.7 x 11.8 x 9.8 in)
U / V travel
±40 mm (±1.57 in)
Our Machines
The Complete EDM (Wire & Sinker) Lineup
Each system is engineered for specific applications. Compare specs to find the right fit.
wire EDM
SW-400
The SW-400 is Sparion's wire EDM platform for die, mold and precision component shops that need to cut hardened tool steel, carbide and exotic alloys without the heat-affected distortion of conventional machining. Automatic wire threading, a 400 x 300 mm work envelope and ±30° taper cutting at 80 mm workpiece height cover everything from simple through-cuts to complex die details. Tollaston installs the SW-400 most often alongside a mold or die-machining department, where wire EDM handles the hardened details a mill can't reach. The deionized-water dielectric system and closed-loop filtration keep surface finish consistent down to Ra 0.1 μm on the best passes, which matters as much for mold polish work as it does for tolerance.
- Max workpiece size
- 650 x 450 x 250 mm (25.6 x 17.7 x 9.8 in)
- Max workpiece weight
- 400 kg (882 lb)
- X / Y / Z travel
- 400 x 300 x 250 mm (15.7 x 11.8 x 9.8 in)
- U / V travel
- ±40 mm (±1.57 in)
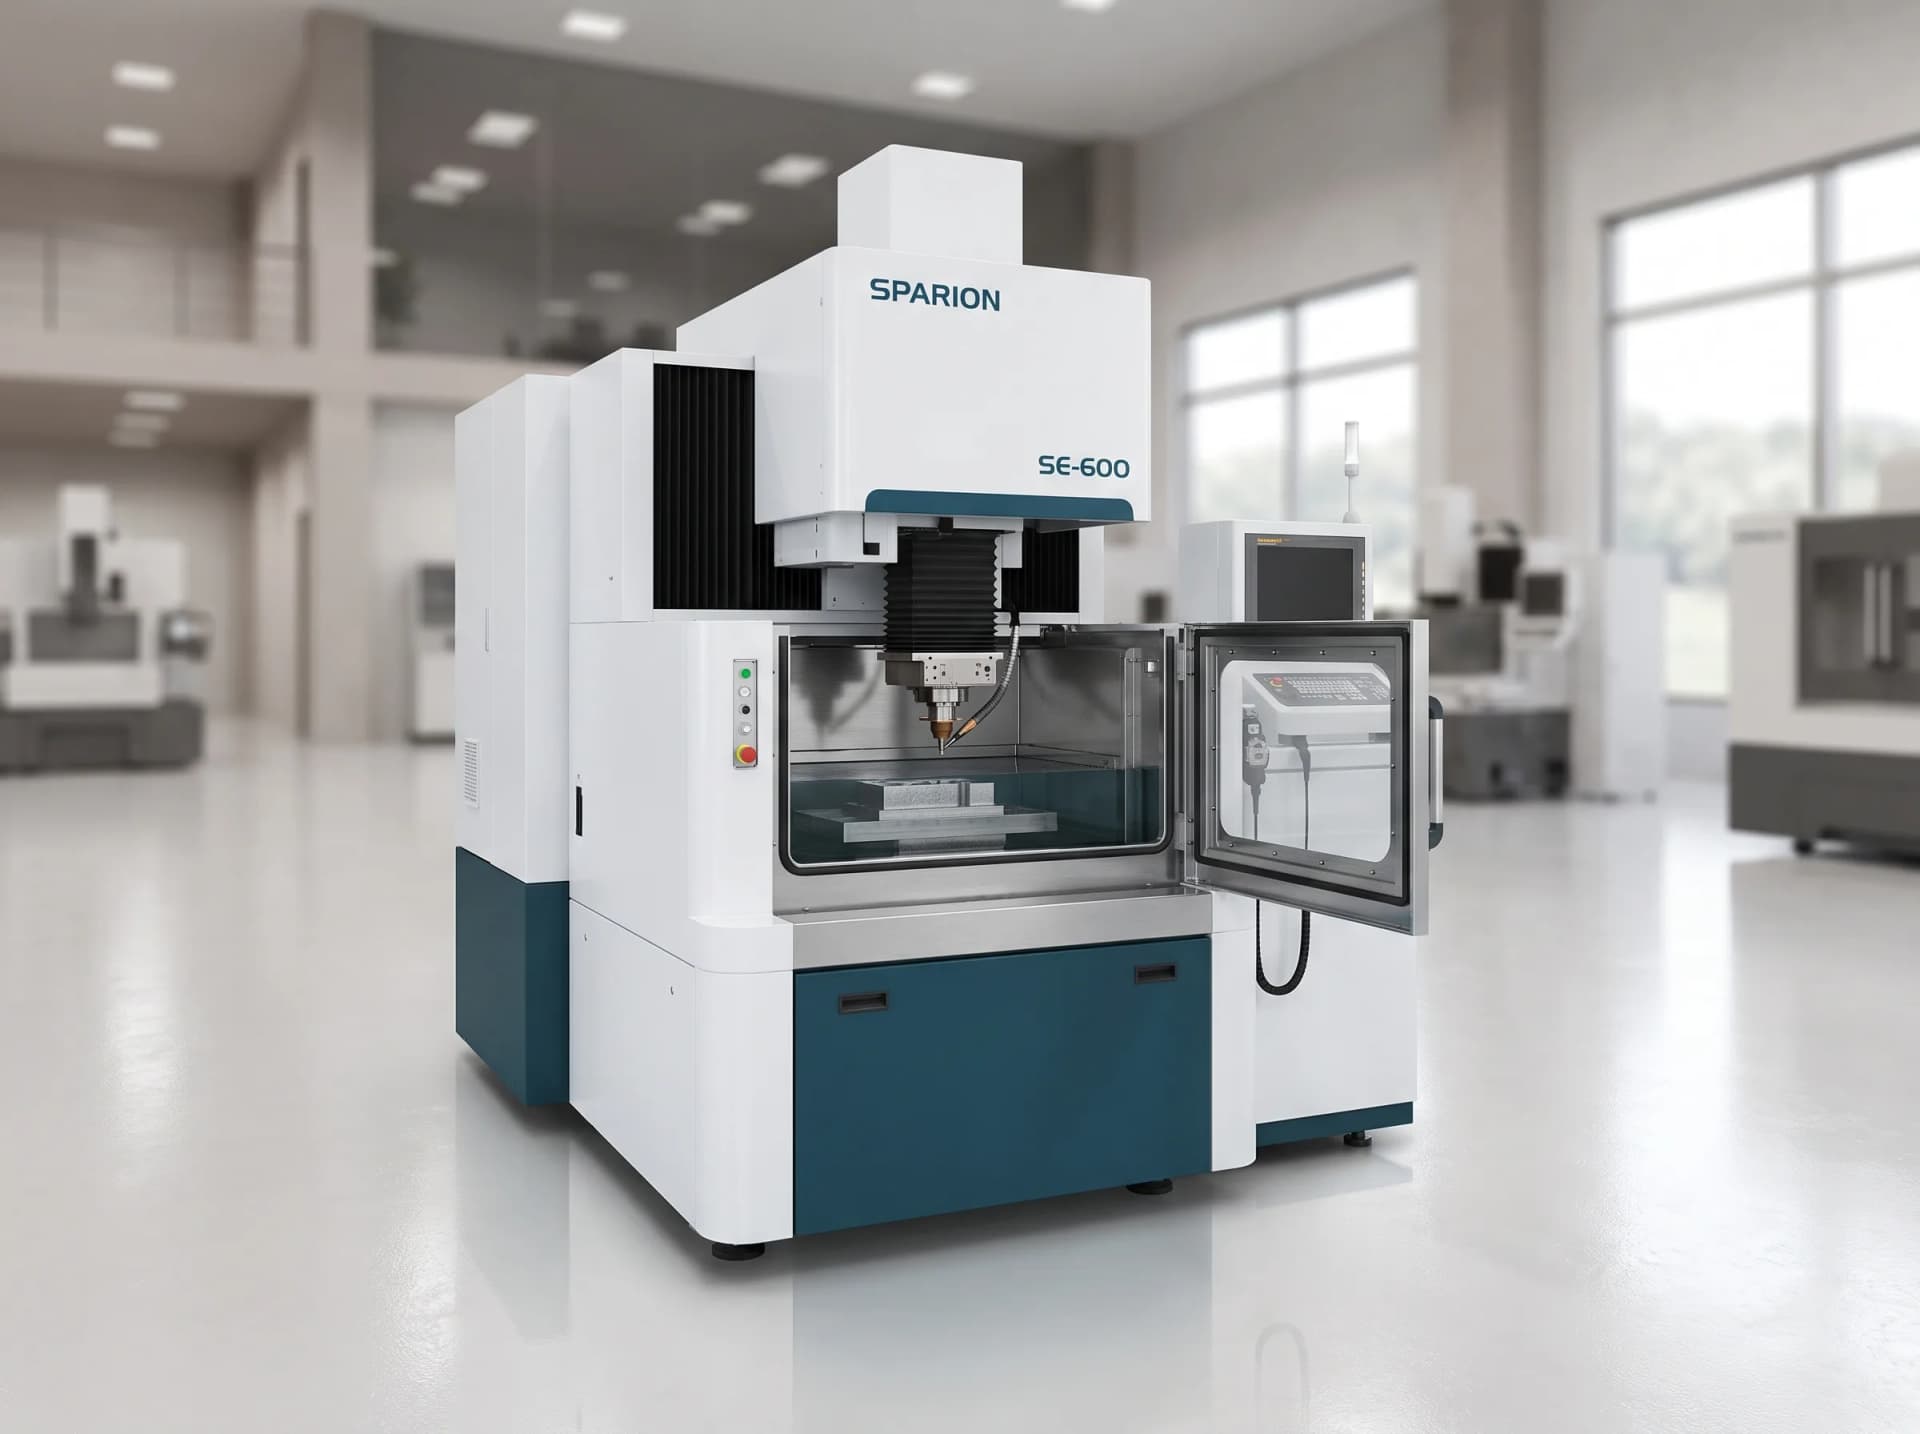
sinker EDM
SE-600
The SE-600 is Sparion's sinker (die-sinking) EDM, purpose-built for burning deep cavities, sharp internal corners and fine surface detail that no cutting tool can reach mechanically. A 400 x 300 x 300 mm travel envelope, a 600 kg workpiece capacity and a 0.1 μm servo head resolution let it hold electrode positioning tight enough for mold cavity and core work at Ra 0.05 μm best finish. Tollaston sells the SE-600 into mold, die and precision tooling shops that need to complement their wire EDM capability with cavity-sinking for closed-end pockets a wire simply can't cut. The oil-based dielectric and automatic level control keep the process stable through long unattended finishing burns.
- Max workpiece size
- 800 x 600 x 400 mm (31.5 x 23.6 x 15.7 in)
- Max workpiece weight
- 600 kg (1,323 lb)
- X / Y / Z travel
- 400 x 300 x 300 mm (15.7 x 11.8 x 11.8 in)
- Max electrode weight
- 50 kg (110 lb)
See everything we carry from Sparion.
Side by Side
Compare Systems
See how each platform stacks up across the specs that matter most.
SW-400Featured
- Process
- Wire EDM
- Max Workpiece
- 650 x 450 x 250 mm
- Dielectric
- Deionized water
- Best Surface Finish
- Ra 0.1 μm
- Positioning Accuracy
- ±0.002 mm
SE-600
- Process
- Sinker EDM
- Max Workpiece
- 800 x 600 x 400 mm
- Dielectric
- Oil-based
- Best Surface Finish
- Ra 0.05 μm
- Positioning Accuracy
- ±0.003 mm
| Specification | SW-400Featured | SE-600 |
|---|---|---|
| Process | Wire EDM | Sinker EDM |
| Max Workpiece | 650 x 450 x 250 mm | 800 x 600 x 400 mm |
| Dielectric | Deionized water | Oil-based |
| Best Surface Finish | Ra 0.1 μm | Ra 0.05 μm |
| Positioning Accuracy | ±0.002 mm | ±0.003 mm |
Applications
Industries We Serve
EDM (Wire & Sinker) systems are trusted across diverse industries and production environments.
FAQ
EDM (Wire & Sinker) Questions
Answers to common questions about our edm (wire & sinker) products.
Electrical discharge machining erodes conductive material with controlled electrical sparks instead of a cutting tool, so it works on hardened steel, carbide and exotic alloys that would destroy a conventional cutting edge, and it leaves no mechanical cutting force to distort thin or delicate sections.
Wire EDM feeds a continuous wire electrode through the part like a bandsaw, ideal for through-cuts and profiles; sinker EDM burns a shaped electrode into the material to create closed-end cavities and fine internal detail that a wire cannot reach.
Most mold and die departments eventually use both — wire EDM for through-cut details and inserts, sinker EDM for cavity and core work — which is why Tollaston sells them as a pair to tooling shops.
The SW-400 achieves Ra 0.1 μm on fine-finish wire passes, and the SE-600 reaches Ra 0.05 μm on sinker finishing burns — both suitable for mold-polish-grade surfaces without secondary polishing in many cases.
On-site training on threading, programming and dielectric system maintenance, plus factory-trained service technicians and stocked spare parts across Canada and the US.
Ready to Discuss Your EDM (Wire & Sinker) Solution?
Our team has 32+ years of experience helping Canadian manufacturers find the right cutting and processing equipment.
32
Years in Business
4,800+
Machines Installed
46
Factory-Trained Technicians
Request a Quote
Tell us about your application and we'll recommend the right machine for your operation.
Financing Available
Flexible payment options on qualifying equipment.
Or email us at [email protected]